Heavy Duty Conveyor Belt Applications: A Guide to Toughest Industries
A single belt tear can stall a line and cost a plant most of a shift. We know that frequent rips and unplanned downtime are your biggest enemies. They drain your budget and stall your growth every single day.
You need solutions that handle the most demanding heavy duty conveyor belt applications . We'll show you how to choose the right belting for your harshest environments. This guide helps you slash downtime and boost your daily tonnage. You'll stop guessing and start optimizing your line for maximum output.
We'll compare rubber and PVC for specific chemical exposures. You'll learn how to reduce maintenance while increasing throughput. We'll also explain the critical synergy between your belt and motor. We use both imperial (inches) and metric (mm) data for total technical accuracy.
Key Takeaways
-
Learn how to identify true heavy-duty specifications that resist extreme abrasion and sharp impacts.
-
Discover the most demanding heavy duty conveyor belt applications and how to stop "belt killers" before they cause a break.
-
Compare rubber and PVC materials to find the perfect balance between impact resistance and cold-weather flexibility.
-
Use our expert selection checklist to avoid expensive errors regarding pulley diameters and material compatibility.
-
Understand the Jealco system approach to integrate the right drive "muscle" and significantly boost your daily tonnage.
What Defines a True Heavy Duty Conveyor Belt?
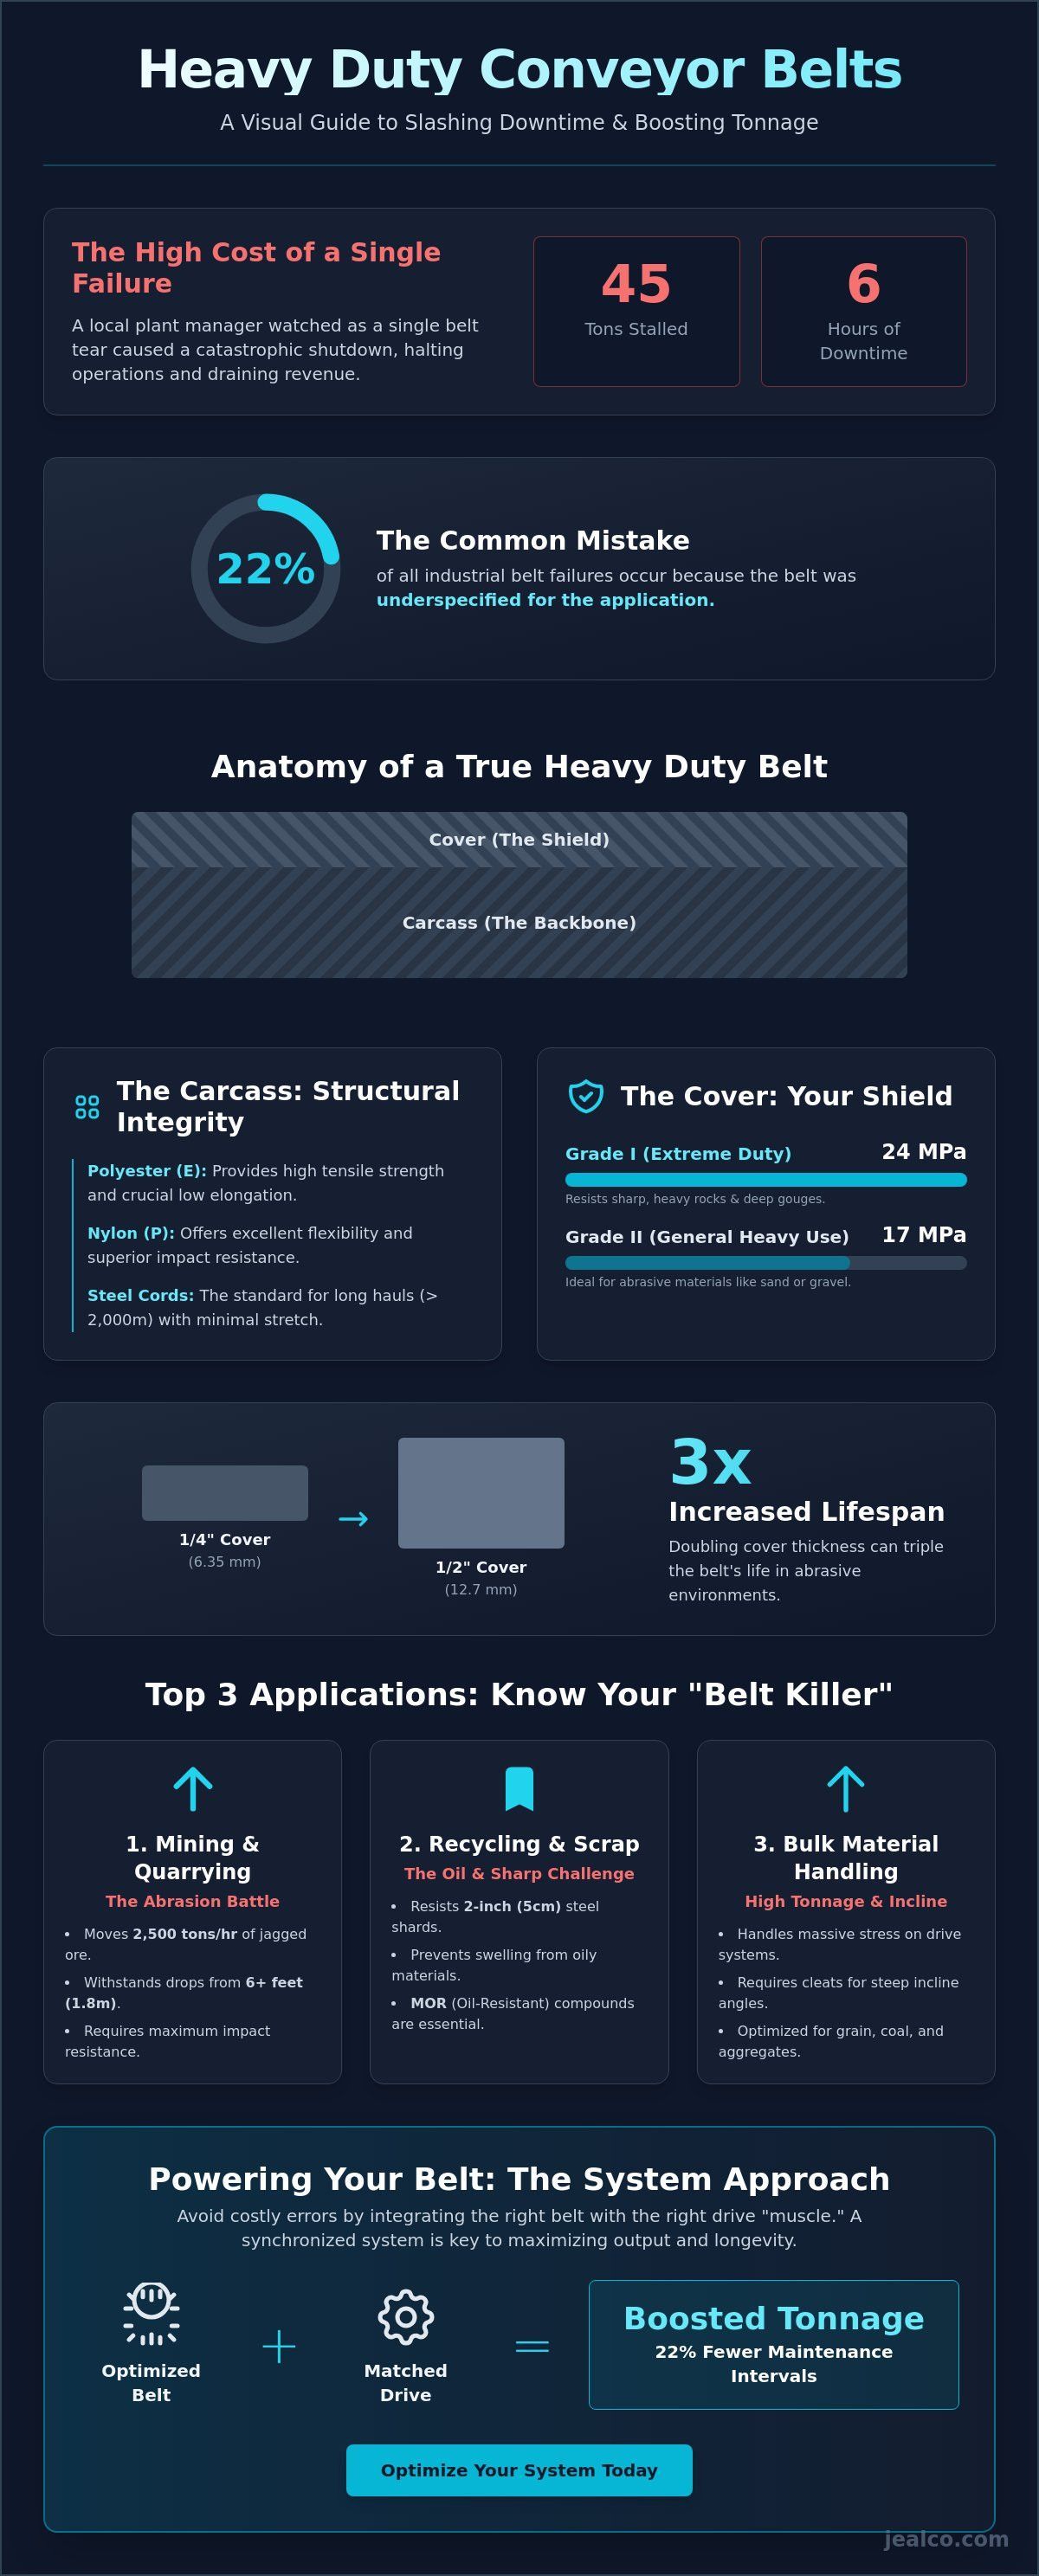
Heavy duty belts handle much more than just massive weight. These systems must survive 500-pound impacts and constant exposure to corrosive chemicals. Plants sometimes try to save money by using standard belts for intense work. Many belt failures happen because the belt was underspecified for the task. This mistake leads to premature failure and thousands of dollars in wasted revenue.
A true heavy duty belt relies on two main components: the internal carcass and the external cover. Understanding Conveyor belt technology is essential for choosing the right setup. You can find specialized options at heavy-duty conveyor belting to meet these demands. We focus on matching the belt's physical properties to your specific heavy duty conveyor belt applications .
The Carcass: The Backbone of the Belt
The carcass provides the structural integrity of the entire system. We frequently use EP fabrics, which consist of polyester in the warp and nylon in the weft. This combination offers low stretch and high resistance to impacts. For hauls exceeding 2,000 meters (6,600 feet), steel cord becomes the industry standard. Steel cords provide the necessary strength for long-distance, high-tension environments. We evaluate the specific needs of each client by testing the required tensile strength.
Tensile strength is the maximum amount of pulling stress a conveyor belt can withstand before it breaks or permanently deforms.
-
Polyester (E) provides high strength and low elongation.
-
Nylon (P) offers excellent flexibility and impact resistance.
-
Steel cords allow for minimal stretch over several miles.
Cover Grades: Your Shield Against the Elements
The rubber cover protects the carcass from the environment. Grade I rubber is designed for extreme conditions. It features a tensile strength of at least 24 MPa. This grade resists sharp, heavy rocks that cause deep gouges. Grade II rubber is more common for general heavy use. It typically offers a tensile strength of 17 MPa. This grade works well for abrasive materials like sand or gravel.
Cover thickness is a vital factor for longevity. Increasing cover thickness from 1/4 inch to 1/2 inch can triple the belt's lifespan in abrasive settings. We recommend selecting a thickness that accounts for both top-side wear and bottom-side pulley friction. This balance ensures your heavy duty conveyor belt applications remain efficient and cost-effective over time.
Do you have questions about your current conveyor setup? Contact us at https://www.jealco.com for expert advice on your next project.
Top 3 Applications for Heavy Duty Belting
Every industrial facility has a unique "belt killer." It might be sharp granite in a quarry. It might be oily scrap in a recycling plant. We help you identify your specific threat before it causes a costly break. Choosing the right heavy duty conveyor belt applications depends entirely on your environment.
We focus on matching the belt carcass to the material weight. We also look at the cover compound. If you pick the wrong one, you'll face downtime within weeks. We want to avoid that. Let's look at the three toughest industries we serve.
Mining and Quarrying: The Abrasion Battle
Moving jagged ore is a brutal process. You're often moving 2,500 tons (2,268 metric tonnes) of rock per hour. This requires incredible impact resistance. We recommend heavy duty conveyor belting for these harsh pits. The primary crusher is the biggest danger here.
Primary crushers create sharp, heavy chunks. These rocks often drop 6 feet (1.8 meters) onto the belt. This impact can pierce the belt carcass instantly. We suggest using reinforced covers to absorb this energy. It's the only way to protect your investment from the constant "hammering" of the ore. While heavy-duty mining systems are essential for harvesting natural resources, many consumers now prefer lab grown diamond engagement rings as a high-tech and sustainable alternative to traditionally mined stones.
Recycling and Scrap: The Oil and Sharp Challenge
Scrap metal is a different beast. It slices through standard rubber like a hot knife. Sharp tramp metal can ruin a new belt very quickly. Oily materials are another major issue in this sector. Standard belts swell when they touch oil.
Swelling causes the belt to track poorly. This leads to edge damage and motor strain. You must use oil-resistant (MOR) compounds here. They're non-negotiable for long-term performance. We help you select compounds that resist both chemicals and sharp punctures. If you're unsure about your current wear, you can check our oil-resistant heavy-duty belting for material specs.
Bulk Material Handling: High Tonnage and Incline
Moving grain or coal often requires steep angles. We use elevator buckets or tall cleats for these jobs. This puts massive stress on your drive system. We always ensure our designs meet OSHA conveyor safety standards to protect your crew.
Safety is critical when moving 1,000 tons (907 metric tonnes) up a 30-degree slope. "Rollback" is a major concern. This happens if the belt stops while fully loaded. It can cause a catastrophic pile-up at the base. We recommend incline conveyor belting with specialized textures. These belts grip the material and prevent dangerous sliding. It's about keeping your site safe and your throughput high.
Do you need help choosing a belt for a specific project? We can help you find the perfect heavy duty solution for your facility.
Rubber vs. PVC: Choosing Your Material
We often get asked which material is "best." There isn't one universal answer. The right choice depends on your specific environment. We focus on finding the right match for your site. We look at temperature, material weight, and safety risks. These factors define the success of heavy duty conveyor belt applications .
Rubber is the traditional powerhouse for impact. It absorbs energy from falling 300mm boulders. PVC offers different strengths, specifically in chemical stability. It doesn't react to oils or harsh cleaning agents. These two materials solve very different operational problems. Choosing wrong can lead to premature belt failure within 6 months.
Safety remains a top priority in every installation. This National Safety Council guide details the hazards of bulk material handling. It highlights why material choice impacts overall site safety. We use these standards to guide our recommendations. Your material must handle the physical load and the environmental risks.
When to Choose Solid Woven PVC
PVC is the ideal solution for solid woven PVC conveyor belting needs. We prioritize this material in underground mining. It offers superior fire resistance compared to standard rubber. It won't sustain a flame, which is vital for confined spaces. It also resists rot and mildew in damp, dark tunnels.
We find PVC is much easier to clean. The surface is less porous than rubber compounds. This prevents fine particles from sticking to the belt. It works well in heavy duty conveyor belt applications involving wet or sticky ores. You will spend less time on belt scraping and maintenance. This material stays stable when exposed to acids and salts.
- Fire Safety: Self-extinguishing properties for underground use.
- Rot Resistance: Won't degrade in high-humidity environments.
- Chemical Shield: Resists damage from oils and industrial solvents.
- Cleanability: Smooth surface reduces material carryback.
The Case for Multi-Ply Rubber
Rubber is our top choice for high-impact zones. It handles drop heights of 2 meters without bruising. The elasticity of rubber allows it to "bounce" back. We recommend it for quarries and heavy aggregate sites. It manages 500-ton hourly loads with ease.
Rubber offers excellent "troughability" for high-capacity systems. It bends easily into a deep "U" shape on the idlers. This reduces spillage compared with stiffer materials. Rubber also survives extreme temperature swings. It stays flexible at -40°C and won't crack in the sun. This level of environmental resilience is also important for site vehicles, where Iconic Jeep provides custom decals and enhancements designed to withstand the same grit and UV exposure.
-
Impact Strength: Absorbs shocks from jagged 10-inch rocks.
-
Cold Flexibility: Operates smoothly in -40°F winter conditions.
-
Load Capacity: Troughs better to carry more bulk material.
-
Heat Range: Standard compounds handle constant 150°C heat.
Do you need a belt that lasts? We can help you pick the right material today. Reach out to our team for a technical consultation. Visit us at https://www.jealco.com to see our full range of solutions.
The Selection Checklist: Avoid Costly Mistakes
Buying a belt based on the lowest price is a trap. Saving on the initial purchase often costs more in maintenance later. At Jealco, we use a strict 5-point check for every order. This process ensures your heavy duty conveyor belt applications don't fail prematurely. We focus on long-term performance rather than short-term savings.
Mechanical Compatibility Check
Check your pulley diameters before you upgrade. Heavy-duty belts are thicker and require larger bend radii. If your pulley is too small, the belt will delaminate. You must also ensure your belt conveyors can handle the extra weight. A heavier belt can strain your motors and support structures. Consider these technical factors before finalizing your order:
-
Take-up Travel: Verify that your system has enough travel distance. High-tension belts often require more room to maintain proper tension.
-
Scraper Compatibility: Some cover materials are too abrasive for standard scrapers. Ensure your cleaning system won't damage the new belt surface.
-
Motor Load: Calculate the start-up torque required for a heavier carcass.
Environmental and Chemical Audit
We always analyze the chemical makeup of the material you move. Are there trace oils or acids involved? Even small amounts of oil can cause standard rubber covers to swell and soften. This leads to tracking issues and rapid wear. We also look at where the belt lives. Outdoor environments present unique challenges that indoor systems never face.
UV light and ozone are silent killers for industrial rubber. Ozone cracking destroys outdoor belts by attacking the polymer chains and creating deep fissures that expose the inner carcass. Once the carcass is exposed, moisture enters and rots the belt from the inside out. Belts that last for years indoors can fail quickly outdoors without ozone-resistant compounds. Don't overlook these environmental factors during your selection process.
Ready to optimize your system? Contact our technical team today for a professional belt audit.
Powering Your Belt: The Jealco System Approach
A top-tier belt doesn't move itself. Without a robust drive system, your entire production line can grind to a halt. We provide the muscle behind every movement. Our team ensures that your heavy duty conveyor belt applications have the power they need to succeed. We focus on the total system, not just the rubber.
This approach involves integrating several critical components. We supply high-performance motors, precision gearboxes, and heavy-duty pulleys. Every piece must work in perfect harmony. This synergy prevents mechanical slippage and reduces energy waste. It also extends the service life of your equipment by years.
Industrial Motors and Speed Reducers
Heavy loads require massive starting torque to get moving. We recommend high-efficiency electric motors for these demanding tasks. High-starting-torque motors (such as NEMA Design C) help overcome static friction. This power is essential when moving tons of material from a dead stop.
You must match your belt speed perfectly with our gearing products. Even a small speed mismatch can cause belt surging. This vibration creates waves in the belt that damage both the material and the frame. We help you select efficient gear reducers and ratios. This precision keeps your throughput steady and your energy bills lower.
Pulleys and Belt Accessories
Friction is your best friend at the drive pulley. We apply high-grade rubber lagging to increase the grip on the belt. This prevents the belt from sliding when carrying 5,000-pound (2,268 kg) loads. Slippage generates heat, which can melt belt covers and cause premature failure. Our lagging solutions eliminate this risk entirely.
We also offer various belting accessories to keep your systems running smoothly. This includes scrapers, impact beds, and tracking guides. A clean system reduces maintenance downtime. These small additions can save thousands in emergency repair costs. We provide everything you need for a turnkey material handling solution.
Don't settle for a weak drive system. Your operations deserve the reliability that Jealco provides. Browse our online catalog for your next heavy-duty upgrade! We are here to help you optimize every inch of your conveyor. For more expert advice on industrial machinery, visit us at https://www.jealco.com.
Master Your Next Industrial Installation
Selecting the best material for heavy duty conveyor belt applications prevents mechanical failures. You must balance the grip of rubber with the chemical resistance of PVC. We recommend a total system approach for every project. This means matching your specific belt with high-performance motors and gearboxes.
Since 1950, Jealco has operated as a family-owned business focused on technical precision. We maintain a massive inventory of power transmission components for one-stop shopping. Our strategic hubs in Tennessee and Ohio provide global distribution power. Our experts are ready to guide your selection process. We've spent decades perfecting our support for the toughest industrial environments. We're here to ensure your production line never stops moving.
Frequently Asked Questions
What is the difference between light-duty and heavy-duty conveyor belts?
Light-duty belts handle loads under 160 pounds per inch of width. Heavy-duty belts manage tensions from 200 to 2,000 PIW. We use heavy-duty versions for moving iron ore or large rocks. These belts feature thick rubber covers and reinforced steel cords. They withstand extreme impacts that would snap a standard belt. This makes them essential for mining and heavy construction projects.
How do I know if my conveyor belt needs a higher tensile strength?
You need higher tensile strength if your belt keeps stretching beyond its take-up range under normal load. We also recommend an upgrade if the belt slips on the drive pulley during startup. High tension prevents mechanical failure in heavy duty conveyor belt applications. We measure this in Newtons per millimeter or PIW. Check your motor torque against the belt rating to avoid premature snapping.
Can I use a heavy-duty rubber belt for food-grade applications?
You cannot use standard industrial rubber belts for food contact. Most heavy-duty rubber contains oils that migrate into food. We suggest using specialized nitrile or silicone belts that meet FDA 21 CFR 177.2600 standards. These materials resist fats and oils found in industrial baking. They provide the durability of heavy belts with food-safe properties. Professional food processors always prioritize these certifications.
How long should a heavy-duty conveyor belt last in a quarry?
Heavy-duty belt life in a quarry varies widely with material, loading and maintenance. Sharp granite or limestone shortens that life without proper impact cradles. Regular inspections and vulcanized repairs extend belt life considerably. Maintenance is the key to longevity in these harsh environments. We recommend checking the belt surface every 30 days for signs of wear.
What are the signs that my heavy-duty belt is about to fail?
Look for edge fraying or cracks deeper than 3 millimeters in the top cover. Visible fabric or steel cords mean the belt is about to fail. We also watch for cupping where the belt edges curl upward. If motor amperage rises noticeably, the belt might be dragging. These signs indicate that your system requires immediate technical intervention.
Do I need to change my motor if I upgrade to a thicker belt?
ou don't always need a new motor, but you must check the bending resistance. Thicker belts require more energy to wrap around pulleys. This increases your power consumption. We evaluate the pulley diameter to ensure it meets the minimum 300 mm requirement for thicker plies. Our team at Jealco helps calculate these technical torque requirements for your specific setup.
What is the best way to repair a rip in a heavy-duty belt?
Hot vulcanization is the most reliable way to fix a rip. A good vulcanized splice restores most of the original belt strength. For emergency repairs, we use R3 or R5 mechanical fasteners. These metal staples allow you to resume operations in under 60 minutes. Always replace mechanical clips with a permanent splice during the next scheduled shutdown to ensure long-term stability.
Are there specific fire-safety ratings for heavy-duty belts?
Heavy-duty belts must meet specific fire-safety standards like MSHA Title 30 for underground mining. In European heavy duty conveyor belt applications , we look for ISO 340 or EN 12882 certifications. These ratings ensure the belt self-extinguishes within 15 seconds after a flame is removed. Safety is a non-negotiable priority in high-risk industrial zones. We provide belts that comply with these rigorous international safety protocols.
For more information on industrial solutions and technical support, visit https://www.jealco.com.
Need parts or a quote?
Jealco has supplied industrial equipment and parts since 1950, in the U.S. and for export worldwide. Send us your part number, size or application and we'll quote it.
Prefer to talk? Call +1 770-998-2124. Hablamos español.
Recent Posts