Food Grade Conveyor Belts for Sale: Your 2026 Buying Guide

Food Grade conveyor belting

Unplanned downtime is expensive for any food processor. We know that finding a reliable food grade conveyor belt for sale often feels like a gamble. You're likely tired of belts that crack under harsh 80°C (176°F) sanitation cycles. Balancing FDA, USDA, and EU regulations shouldn't be your full-time job.

We've spent decades solving complex thermal and bakery process challenges. We'll show you how to select FDA-compliant materials that withstand your specific cleaning chemicals. You'll learn to maximize uptime and lower your total cost of ownership. We want to help you raise equipment effectiveness through better component selection.

This guide breaks down the technical differences between TPU and modular plastic options. We also provide a checklist for 2026 safety standards. Let's ensure your production line stays efficient and compliant. Visit us at https://www.jealco.com to see how we support your operational success.

Key Takeaways

  • Learn to distinguish between food contact types. We help you meet FDA standards and save money.
  • We compare PU, PVC, and silicone. Discover the right polymer to prevent premature belt failure.
  • Simplify your search for a food grade conveyor belt for sale. We list the specs you need for a perfect fit.
  • Avoid common cleaning mistakes. We share tips to maximize your equipment’s lifespan and hygiene.
  • Match your belt to your processing stage. We help you pick the best antimicrobial surfaces.

What Exactly Makes a Conveyor Belt 'Food Grade'?

We define food-grade belting as materials safe for direct contact with human food. These specialized materials won't migrate harmful chemicals into your product. Food-grade belts are non-toxic, non-absorbent, and resistant to bacterial growth.

Distinguishing between direct and indirect contact is vital for your budget. Direct contact belts touch the food directly. These require expensive, high-purity polymers to prevent contamination. Indirect contact belts might only carry sealed boxes or crates. Choosing the right food grade conveyor belt for sale prevents overspending on unnecessary specs. You don't need a medical-grade belt for cardboard boxes.

A standard conveyor belt used in a warehouse isn't safe for a bakery. The FDA and USDA set these strict safety rules. They ensure your equipment doesn't contaminate the food supply. We see these standards as essential for consumer safety and operational success. These regulations protect both the manufacturer and the end consumer.

FDA 21 CFR 177.2600 Explained

FDA 21 CFR 177.2600 is the gold standard for rubber and plastic components. It identifies which ingredients are safe for repeated food contact. The 2026 update specifically targets "forever chemicals" or PFAS. Manufacturers must now certify their belts are PFAS-free to meet modern safety codes. Don't take a supplier's word for it. Always demand a Certificate of Compliance (CoC) with every order. This document is your shield during health inspections and safety audits.

USDA and 3-A Sanitary Standards

USDA standards focus on the "cleanability" of the entire system. Meat and poultry plants face much tougher rules than dry goods processors. A "washdown-ready" belt isn't always USDA-approved for raw protein. Raw meat requires non-porous surfaces to stop bacterial growth like listeria. Look for the 3-A symbol on food grade conveyor belting products. This symbol means the belt meets strict sanitary design criteria. It ensures the material handles 80°C (176°F) water at high pressure. Most bakery belts are 3mm (0.12 inches) thick to balance flexibility and strength. When browsing a food grade conveyor belt for sale , check the 3-A rating first.

Need expert advice on your next installation? Visit us at https://www.jealco.com to see our full range of solutions.

Comparing Materials: PU vs. PVC vs. Silicone Belts

Buying the wrong material is a common mistake. Plants often pick the lowest price. This mistake costs more in the long run. A cheap belt might fail in 90 days. A correct one lasts for years. When looking for a food grade conveyor belt for sale, you must match the polymer to your product. Switching to the right material avoids costly downtime.

Thermoplastic Polyurethane (TPU or PU) is the gold standard. It provides excellent resistance to vegetable oils and animal fats. It doesn't swell or crack easily. PVC belting is a cost-effective choice. It works best for fruit, vegetables, and dry goods. In 2026, food safety audits are stricter than ever. Choosing the right material is a compliance requirement, not just a preference.

When to Choose PU Over PVC

PU generally offers better abrasion resistance than PVC. We recommend it for high-fat meat processing. It stays flexible at temperatures as low as -30°C (-22°F). This makes it perfect for frozen food lines. PVC can become brittle and crack at these temperatures. These cracks harbor bacteria and ruin your hygiene scores. For lighter applications, you can explore our light-duty conveyor belting options.

PU is also non-porous. This prevents the absorption of odors and colors. If you process beets or berries, PU won't stain like PVC. PU belts generally last longer than PVC in oily environments. This durability justifies the higher initial cost. It keeps your line running without frequent replacements.

Silicone and Specialized Coatings

Bakery items often come straight from the oven. They are hot and very sticky. Silicone belts handle continuous temperatures up to 200°C (392°F). They have a unique "release" property. This prevents dough or sugar from sticking to the surface. You must follow strict Regulations for Food Processing and Safety when choosing these coatings. These rules ensure your equipment doesn't contaminate the food supply.

Silicone is softer than PU or PVC. It requires specialized tracking and tensioning accessories to prevent slipping. Silicone's release properties can reduce product waste in bakeries. The non-stick surface ensures every cookie or pastry stays intact. If your product is high-sugar or high-heat, silicone is your best bet.

Choosing the right food grade conveyor belt for sale depends on your specific environment. We provide technical audits to ensure your choice matches your operational needs. You can view our full range of technical specs in our online catalog to find the perfect fit for your facility.

Matching Your Belt to Your Food Processing Application

We group food applications into three main categories. These are Raw, Processed, and Packaged. Each environment has unique demands. Choosing the right food grade conveyor belt for sale depends on your specific product. The wrong choice is a common cause of unplanned downtime in new facilities.

Raw proteins require antimicrobial surfaces to prevent bacteria growth. Bakery and confectionery lines must manage flour dust and high heat. Fruit and vegetable processing involves high moisture and acidic runoff. All materials must comply with FDA regulations for food contact materials to ensure consumer safety.

The Raw Protein Challenge

Hygiene is the top priority for meat and poultry. We recommend blue belts for these lines. The blue color provides a sharp visual contrast. It helps workers spot foreign plastic fragments quickly. This prevents contaminated products from reaching the market.

  • Homogeneous belts: These are solid plastic. They don't have fabric layers. This prevents delamination in wet environments.
  • Sanitation: These belts withstand high-pressure washdowns. They resist caustic chemicals used during nightly cleaning cycles.
  • Durability: Solid belts don't fray. This keeps fibers out of your food stream.

Dry Goods and Packaging Lines

Bakery environments face different risks. Flour dust can lead to static buildup. We provide belts with anti-static properties. This reduces the risk of dust explosions in grain facilities. It also keeps the line running smoothly without shocks.

Sticky residues from sugar or dough are common. We use non-stick coatings to improve release. For finished goods, you often need to move items between levels. We suggest using incline conveyor belting for these tasks. These belts feature rough-top textures or cleats. They keep bagged goods from sliding back down the line.

We focus on robust solutions for every stage. Our team ensures your food grade conveyor belt for sale meets 2026 industry standards. We prioritize technical precision and long-term reliability. This approach protects your equipment and your reputation.

Do you have questions about your specific application? We're here to help you optimize your production line. Contact us today to discuss your technical requirements. You can find more details at https://www.jealco.com.

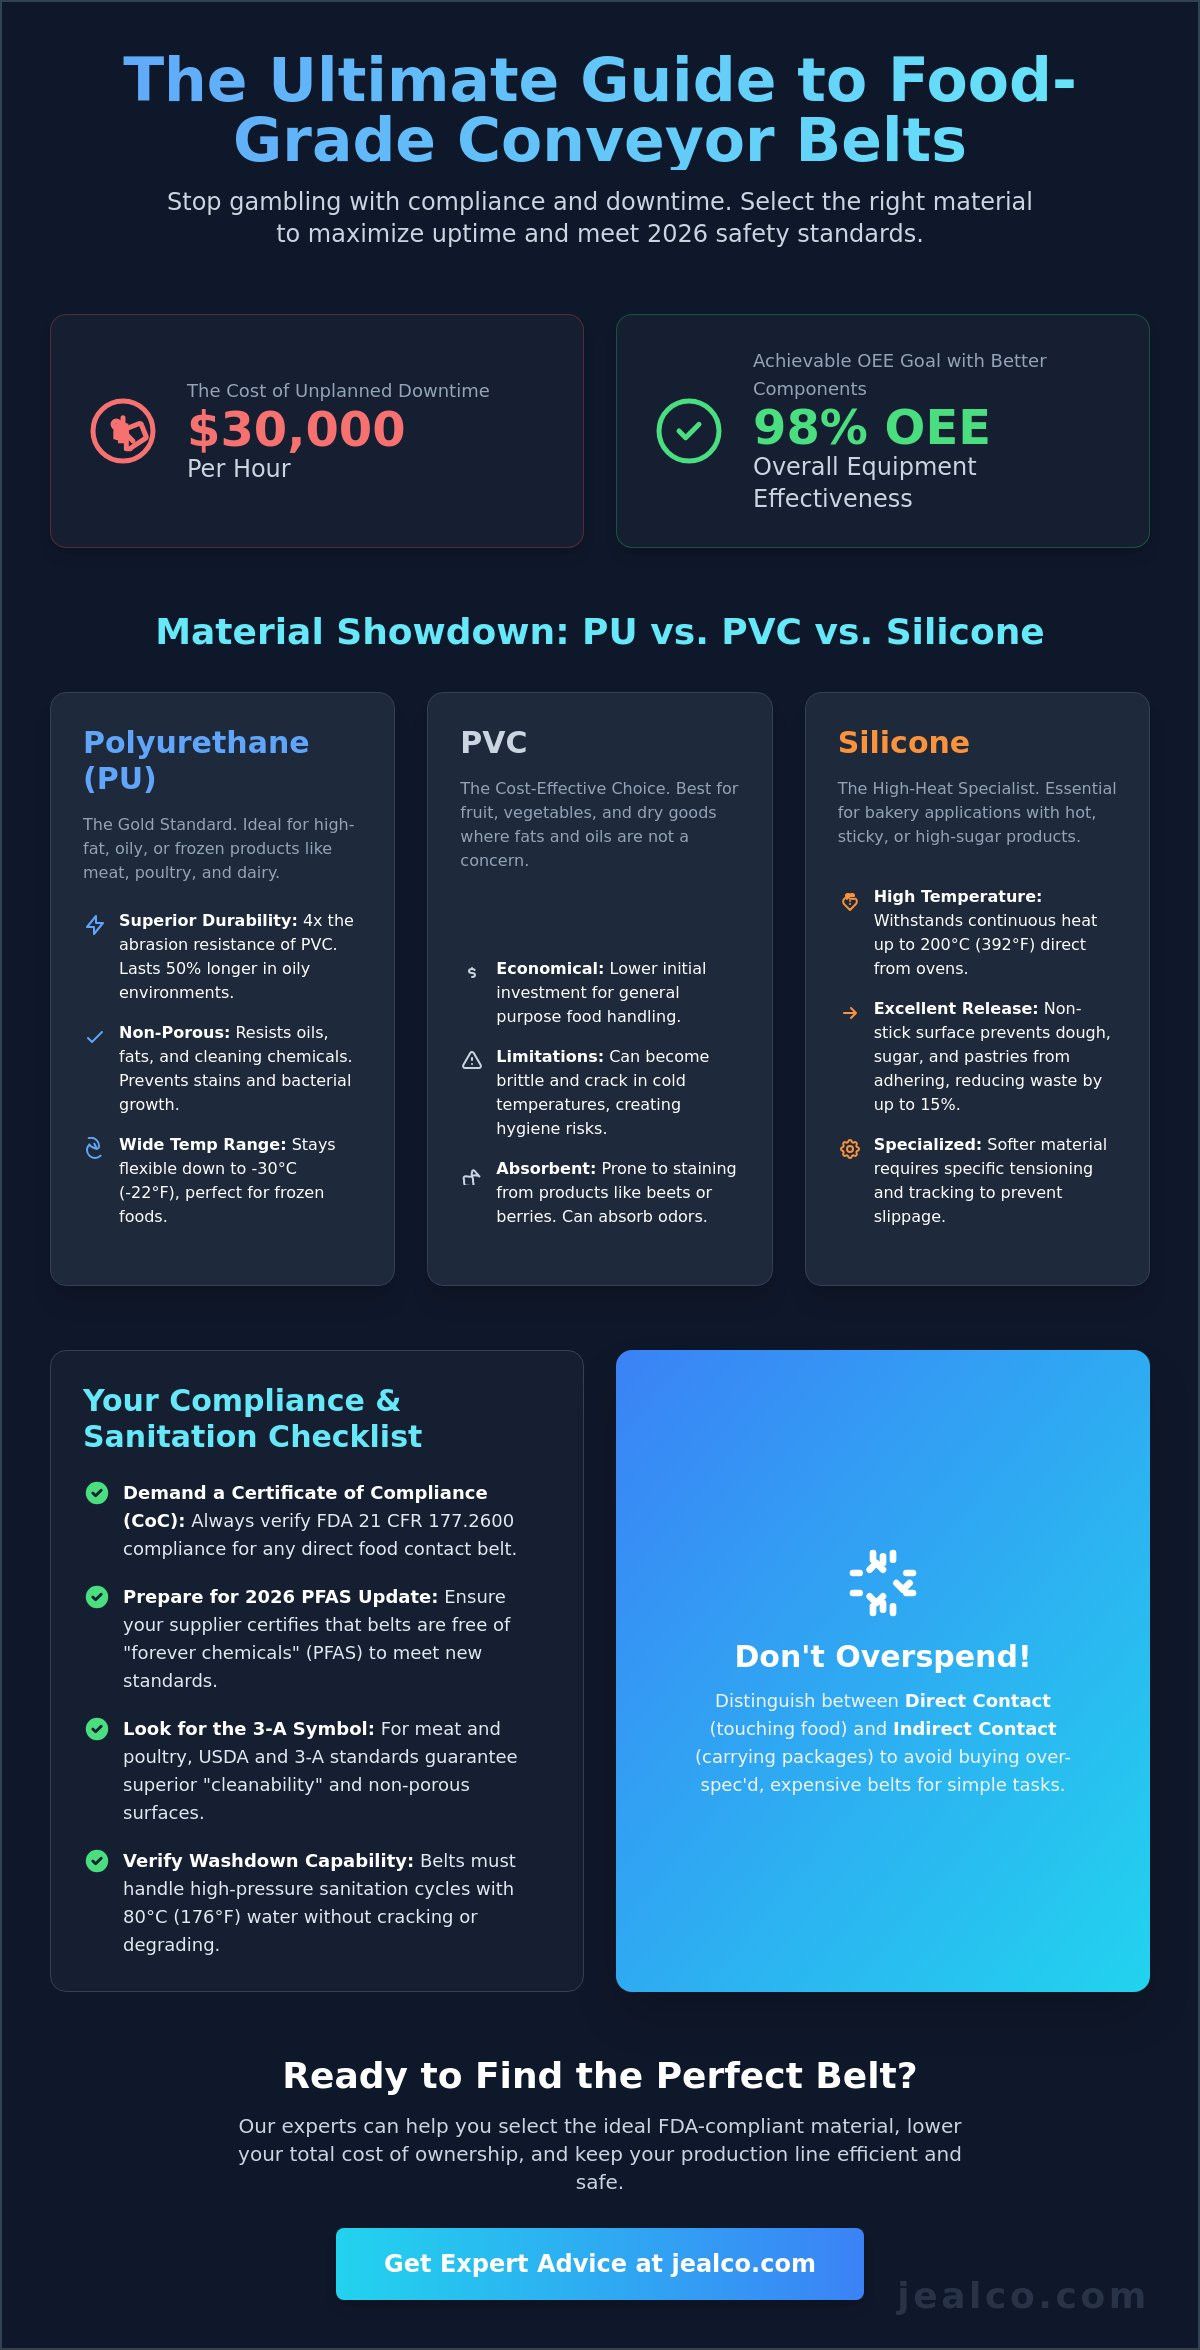
Infographic about food-grade conveyor belts

Maintenance and Sanitation: Maximizing Belt Lifespan

We've analyzed years of maintenance logs across the food processing industry. Improper cleaning protocols are a common cause of belt failures. You can avoid these costly shutdowns with a proactive strategy. We focus on technical precision to keep your lines running. Proper sanitation does more than meet safety codes. It extends the physical life of every food grade conveyor belt for sale in your facility.

Cleaning Chemical Compatibility

Polyurethane (PU) belts are industry standards. However, they react differently to various sanitizers. Chlorine-based cleaners are powerful but aggressive. They can degrade PU surfaces over time. Quaternary ammonium sanitizers are often a safer choice for belt integrity. We also see "hydrolysis" in hot, humid environments. This occurs when moisture breaks down polymer chains. It makes the belt brittle and prone to cracking. We recommend checking your belting accessories for rust or signs of chemical wear. Corroded fasteners or pulleys can easily transfer contamination to a brand-new belt.

Clean-in-Place (CIP) systems offer efficiency. But you must calibrate them for your specific polymer. High-pressure sprays can delaminate lower-quality belts. We suggest using a wide-angle nozzle at 20 bar (290 psi) to prevent surface scarring. This keeps the belt smooth and easy to sanitize.

Tracking and Edge Protection

Misalignment is a silent killer of industrial equipment. We call this "tracking" issues. If a belt shifts just 5 millimeters (0.2 inches), it may rub the frame. This causes edge fraying. These loose fibers are a major physical contamination risk. Edge sealing is the best way to prevent bacteria wicking. This process closes the porous fabric core of the belt. It stops liquids from soaking into the internal layers. We prioritize this feature for every food grade conveyor belt for sale to ensure long-term hygiene.

Daily Inspection Checklist

  • Surface Integrity: Look for nicks or gouges. Bacteria hide in these small cuts.
  • Belt Tension: Avoid over-tensioning. It kills your motors and bearings. Aim for the minimum tension required to prevent slipping.
  • Structural Shape: Monitor for "cupping" or "bowing." This happens on wide belts under stress. It ruins product alignment.
  • Scraper Alignment: Ensure scrapers aren't digging into the belt surface.

Consistency is key. A five-minute check every morning saves hours of downtime later. Small adjustments can prevent total system failures. We believe in building solutions that last through rigorous cleaning cycles.

Need expert advice on maintaining your system? Contact Jealco today for professional technical support.

Ready to Order? How to Source the Right Belt Today

We make finding a food grade conveyor belt for sale simple. Our team focuses on your specific line specs to avoid costly downtime. We don't just sell parts; we provide solutions backed by industrial experience since 1950. This history allows us to identify potential issues before they stop your production line.

To get started, we need a few key details from your facility. Please have your belt width and total length ready. We also need the material type and your pulley diameters. These metrics ensure the belt tracks perfectly on your existing frames and handles the required tension.

Buying from a specialized distributor like Jealco beats a general marketplace every time. Marketplaces often lack the technical support needed for complex food processing environments. We use our 70-year history to ensure you get the right part the first time. This precision avoids the failures common with generic, unverified suppliers.

Custom Fabrication Options

Choosing the right splice is vital for food safety. Endless belts are the gold standard for hygiene. They eliminate crevices where bacteria grow. Mechanical fasteners are easier to install, but they require more frequent cleaning protocols to meet 2026 safety standards.

  • Cleats: These help move products up steep inclines without slippage.
  • V-guides: These ensure your belt stays centered during high-speed runs.
  • Sidewalls: These prevent small food items from falling off the edges.

You can browse these specific configurations in our online catalog to see what fits your production goals.

Getting a Fast Quote

We know a broken line costs money every minute it sits idle. Our team commits to rapid responses for emergency line-down situations. We respond quickly to keep your facility moving.

We also handle the complex logistics for you. Our experts manage international shipping and exports to over 30 countries. We ensure all customs documentation meets current 2026 regulatory standards for industrial machinery. This global reach ensures your parts arrive regardless of your location.

Ready to upgrade your system with a reliable partner? Contact us today at Jealco to speak with a belting expert about your specific needs.

Secure Your Production Efficiency for 2026

Choosing the right material is the first step toward a seamless operation. Switching from standard PVC to PU or silicone significantly reduces contamination risks. Proper sanitation isn't just about safety; it's about protecting your equipment's lifespan. Following a strict cleaning schedule helps your belts last longer and perform better under pressure.

We've provided expert technical support to the food industry since 1950. Our team ensures every component meets strict FDA and USDA compliance standards. With shipping hubs located in Tennessee and Ohio, we deliver the parts you need without long wait times. We focus on durability so you can focus on growth.

Finding a reliable food grade conveyor belt for sale doesn't have to be a challenge. We have the technical knowledge to match a belt to your specific processing environment. Whether you handle delicate pastries or heavy proteins, we'll help you find the right solution for your 2026 goals.

We look forward to helping you optimize your facility and keep your lines moving with confidence.

Frequently Asked Questions

Is blue color mandatory for food-grade conveyor belts?

Blue is not legally mandatory, but it is the industry standard for safety. Blue provides high visual contrast against most food products. This helps operators detect a 1 mm fragment of belt material if it breaks off. FDA regulations do not mandate blue, but many plants prefer it. We recommend blue to help you meet GFSI audit requirements easily.

Can I use a standard industrial belt for packaged food?

You shouldn't use standard belts even for packaged goods. Standard belts often contain chemicals like phthalates that can migrate through thin packaging. Buying a certified food grade conveyor belt for sale ensures you meet FSMA 204 safety standards. We provide belts that comply with EC 1935/2004 for all food contact surfaces. This protects your brand from contamination risks and potential product recalls. To see how these safety standards support high-quality food innovation, learn more about Jolloful and their mission to deliver authentic flavors globally.

What is the difference between FDA-compliant and FDA-approved?

The FDA does not actually approve conveyor belts; they set standards for compliance. Manufacturers must ensure their materials meet FDA Title 21 CFR 177 requirements for food contact. We provide full documentation proving our materials are compliant. This means the belt is safe for direct contact with food during production. It ensures your facility stays in line with current 2026 health and safety regulations.

How often should I replace my food-grade conveyor belt?

Most belts last 12 to 36 months depending on your specific application. In high-heat bakery environments, you might see wear after 18 months of use. We suggest inspecting for fraying or surface cracks every 30 days. Replacing a belt before it fails prevents unplanned downtime during peak shifts. Proper maintenance and tracking adjustments extend this lifespan.

Are modular plastic belts better than fabric belts for food?

It depends on your specific drainage and cleaning needs. Modular belts offer better drainage for washed produce or raw meat. Fabric belts provide a smooth surface that prevents dough from sticking in bakery lines. We evaluate your 2026 production goals to help you choose the right material. Each option has specific benefits for different parts of your processing facility.

Do you offer antimicrobial conveyor belts?

Yes, we provide belts with silver-ion additives that inhibit bacterial growth on the belt surface. They help reduce biofilm formation between cleanings. They are especially effective in meat processing where Listeria risks are high. This technology reduces the chemical load needed during your sanitation cycles.

Can I install these belts myself or do I need a specialist?

You can install mechanical fastener belts yourself, but vulcanized belts require a specialist. Have a qualified splicing crew make the joint to ensure a seamless result. A professional install prevents tracking issues, a common cause of premature belt failure. We offer 24/7 support for all installations. This ensures your line starts up without any tracking errors or tension problems.

What temperature range can a silicone food belt handle?

Silicone food belts typically handle temperatures from -54°C to 260°C (-65°F to 500°F). This makes them ideal for cooling tunnels or industrial ovens. These belts are designed to stay flexible under continuous high-heat exposure within their rated temperature. Their non-stick properties stay active across this entire thermal range. This durability makes them a top choice for a food grade conveyor belt for sale.

For more technical specifications and expert guidance on your production line, visit us at https://www.jealco.com.

Share this article

Need parts or a quote?

Jealco has supplied industrial equipment and parts since 1950, in the U.S. and for export worldwide. Send us your part number, size or application and we'll quote it.

Prefer to talk? Call +1 770-998-2124. Hablamos español.

Recent Posts

Three technicians review a drawing beside an open helical speed reducer, loose gears and bearings on
By Jealco International, Inc. • September 24, 2026
Compare mechanical and thermal ratings, apply AGMA service factors, and cross-reference obsolete gearboxes with an independent speed reducer supplier.
By Mark Lacefield • September 17, 2026
Why "we apologize for any inconvenience" minimizes real customer problems, where the word came from, and what to say instead to build trust with industrial clients.
Two engineers with a tablet beside an inclined conveyor carrying crushed aggregate
By Jealco International • September 14, 2026
Calculate belt conveyor horsepower with CEMA 7th Edition formulas — effective tension, drive efficiency, and a worked 7.5 HP example from Jealco International.
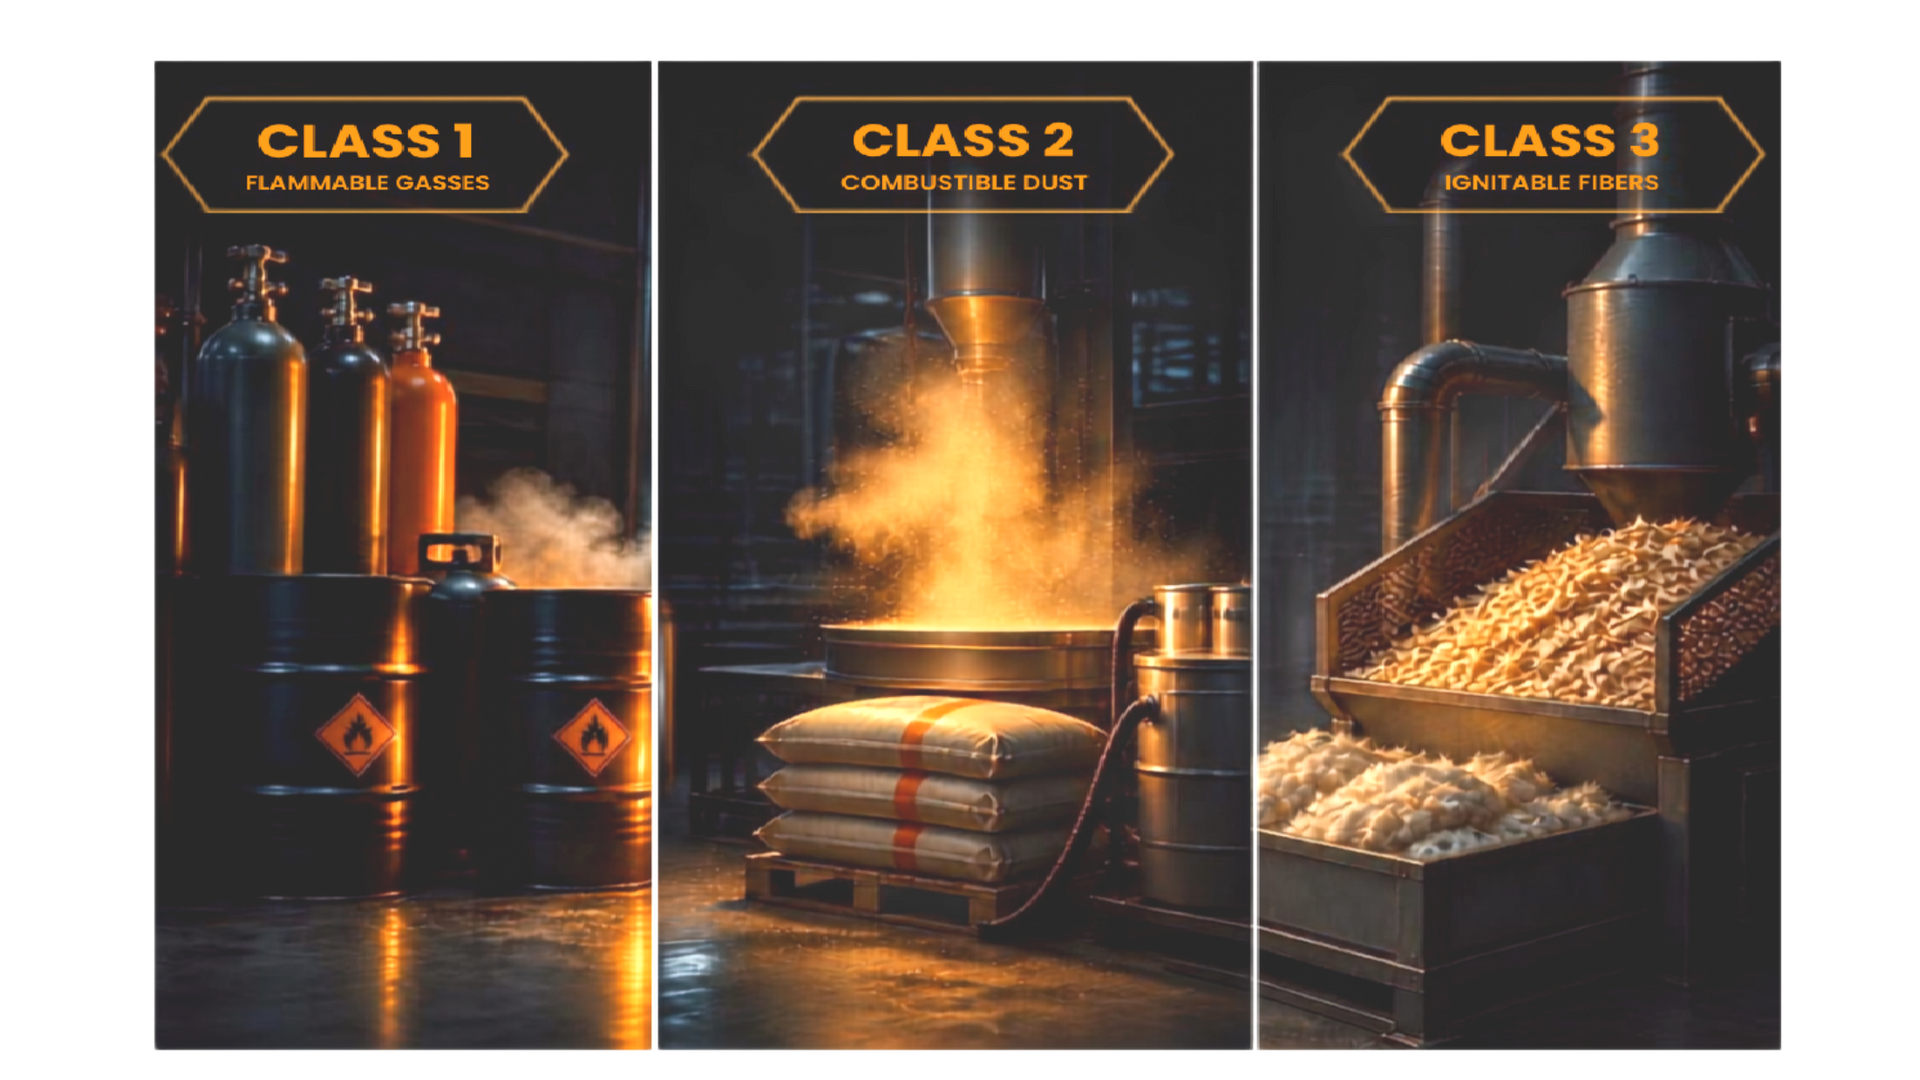
photo depicting various hazardous classes such as  flammable gas, dust, or ignitable fibers
By Jealco International, Inc. • September 1, 2026
Choosing industrial motors for hazardous locations: Class and Division versus IEC Zone ratings, explosion-proof versus dust-ignition-proof, and dual certification.
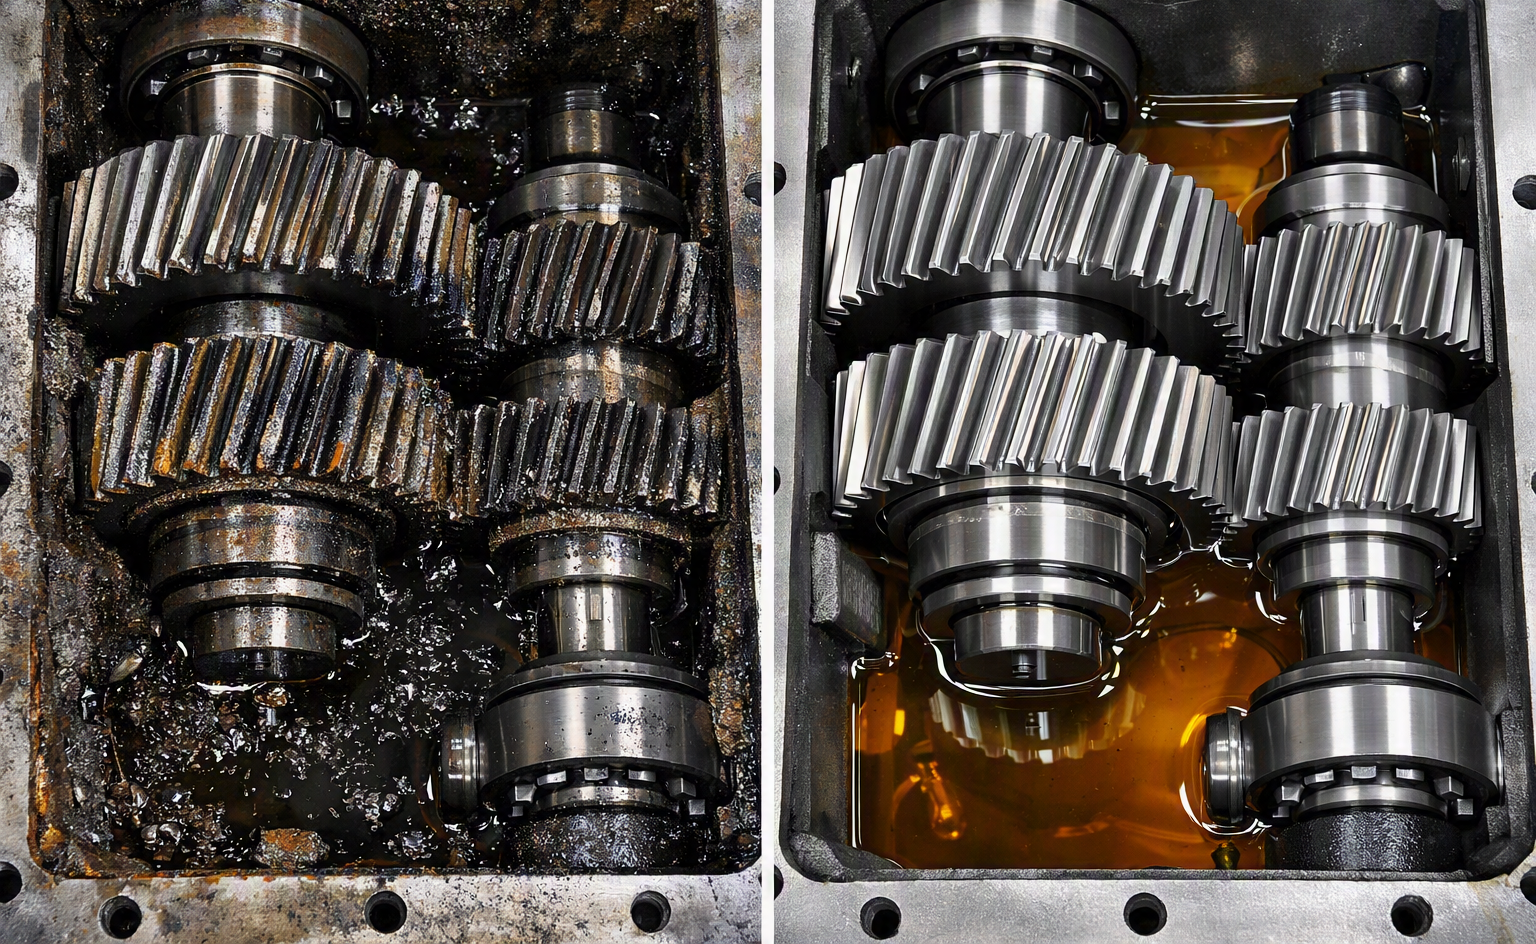
image of speed reducer gears in an enclosed container showing worn versus well-maintained gears
By Jealco International, Inc. • August 24, 2026
Speed reducer lubrication best practices: choosing the right viscosity, matching the oil to worm or helical gearing, and using oil analysis to catch wear early.
Gloved hand holding a non-sparking beryllium copper wrench over assorted wrenches and socket bits on a dark workbench
By Jealco International, Inc. • August 17, 2026
Avoid catastrophic failure with the right non-magnetic hand tools. Our guide helps you compare alloys, prevent contamination, and streamline global sourcing.
Three white elevator buckets stacked with flour against a dark rustic background
By Jealco International, Inc. • August 10, 2026
Boost throughput with proper elevator bucket venting for fine materials. We show you how to eliminate air pillows, reduce dust, and meet NFPA 660 standards.
technicians evaluating a piece of equipment in a grain processing facility
By Jealco International, Inc. • August 3, 2026
Sourcing non-sparking conveyor and elevator components: bronze and beryllium-copper alloys, static control, and what makes a part safe for explosive dust.
Person at computer reviewing cost estimates for a conveyor system
By Jealco International, Inc. • July 27, 2026
Your conveyor quote is not your final cost. See how freight, duties, crating and lifecycle expenses shape the real budget, and how to avoid OEM parts markups.
Stainless steel sanitary conveyor with open-frame design and washdown-rated motor for food processing environments.
By Jealco International, Inc. • July 20, 2026
Learn the engineering principles for sanitary conveyor design for food processing. We'll show you how to meet FSMA rules and cut cleaning time.
Industrial roller chain and sprocket drive on a conveyor system, illustrating proper tension for maximum service life.
By Jealco International, Inc. • July 13, 2026
Master how to properly tension a roller chain using the 2% slack rule, precision alignment steps, and detailed failure diagnostics to maximize drive service life.
Industrial conveyor belt running through a high-heat processing zone, illustrating the thermal stres
July 6, 2026
Compare high temperature resistant conveyor belting options like EPDM, silicone, and Kevlar to prevent thermal hardening and unplanned heat-related downtime.
Show More